ASME standard nitrogen generators refer to nitrogen production equipment
whose pressure vessels and pressure-bearing components are manufactured in
accordance with the ASME Boiler and Pressure Vessel Code. Most of them adopt
Pressure Swing Adsorption (PSA) technology. Equipment procurement is only a
one-time upfront investment. Consumptions during operation constitute the core
factor determining the total life-cycle cost. When calculating the cost of an
ASME standard nitrogen generator, it is insufficient to simply compare equipment
quotations. A comprehensive calculation covering compressed air energy
consumption, consumable replacement, maintenance, spare parts, labor and gas
leakage losses across operation dimensions is required to estimate long-term
operating expenditure and optimize operation strategies.
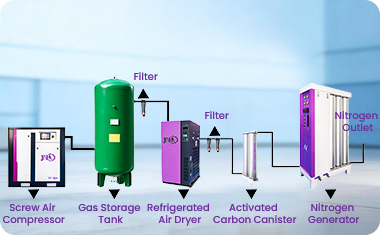
The largest operating expense comes from compressed air power consumption.
The PSA nitrogen generation process consumes large volumes of compressed air to
produce nitrogen, with air consumption normally 2 to 3 times the nitrogen
output. Continuous power draw of air compressors ranks as the primary component
of operating cost. Pressure vessel shells built to ASME standards undergo
rigorous strength verification. Their reliable pressure tolerance enables stable
long-term operation within optimal adsorption pressure ranges and helps reduce
air consumption. Oversized units force air compressors to run under low load,
raising power consumption per unit nitrogen. Conversely, continuous overload
operation increases pressure fluctuations, accelerates wear of valves and seals
and pushes up maintenance costs. During operation, stabilizing supply pressure,
fixing pipeline leaks and cutting unnecessary air venting effectively reduce
electricity use and control operating expenses.
Consumable replacement creates recurring operating costs, mainly including
filter cartridges, sealing elements and carbon molecular sieves. The
pre-treatment filter system protects carbon molecular sieves inside adsorption
towers. Primary, oil-removal and water-removal filter cartridges gradually clog
under continuous operation as differential pressure rises and must be replaced
periodically. Delayed replacement allows oil and moisture to enter adsorption
towers and permanently poison carbon molecular sieves, which are high-cost
consumables. The ASME pressure vessel shell itself has a long service life and
rarely needs replacement. However, fluororubber gaskets at flanges and valve
joints age under repeated pressurization and depressurization cycles, losing
elasticity and developing micro-leaks, requiring regular inspection and
replacement. Consumable service life is strongly related to compressed air
quality. Cleaner compressed air extends the service life of filters and
molecular sieves and reduces consumable costs. During daily operation, maintain
consumable logs and plan procurement in advance to avoid premium emergency
purchases.
Inspection and preventive maintenance are essential to sustain stable
operation and avoid expensive emergency repair bills. Pressure-bearing
components built to ASME codes require periodic examinations during service to
inspect welds, wall thickness, corrosion and flange sealing surfaces. Routine
preventive maintenance includes valve function tests, pipeline tightness checks,
control system calibration and oxygen analyzer verification. Although preventive
maintenance increases short-term operating spending, it detects hidden risks
such as micro-leaks, valve sticking and declining molecular sieve performance in
advance and prevents unplanned shutdowns. Production losses caused by unexpected
downtime are often far higher than maintenance fees. For continuous-process
plants, the operation strategy focuses on preventive maintenance to reduce
unplanned outages and control overall operating costs.
Spare part inventory and operation labor costs cannot be overlooked.
Valves, sensors and analyzers matched to ASME standard nitrogen generators
require safety stock. Insufficient spare parts prolong downtime when faults
occur, while excessive inventory locks up working capital and raises storage
costs. Labor cost depends on inspection frequency and equipment automation
level. Modern nitrogen generator units use PLC intelligent control systems to
monitor nitrogen purity, pressure, flow and tower conditions in real time with
automatic fault alarms, cutting manual on-site supervision time. Higher
automation reduces routine inspection workload and labor expense. Operators only
need to log operating parameters, check differential pressure and cabinet
conditions and complete simple consumable changes.
Pipeline losses and gas leakage represent hidden operating costs that are
easily ignored. Even if the main unit meets ASME standards, leaks in gas
pipelines and flange joints waste finished nitrogen and increase production cost
per cubic meter of nitrogen. Over long runtimes, pipeline corrosion and gasket
aging trigger leaks. Therefore regular tightness testing and prompt leak repairs
are required during daily operation to reduce nitrogen waste. Pipeline thermal
insulation and moisture protection protect pipework, slow corrosion and lower
leakage risks.
Operating costs vary with working conditions. Changes in equipment load and
ambient temperature and humidity alter air consumption and consumable aging
rates. Under intermittent low-load production, a sleep mode can be activated to
reduce no-load power consumption of air compressors. For full-load continuous
production, upstream air purification must be strengthened to protect core
adsorbent materials. Many factories only focus on purchase price and ignore
operating cost differences under varying operating conditions, leading to
overspending in later operation.
The total operating cost of an ASME standard nitrogen generator sums up
energy consumption, consumables, inspection, spare parts and leakage losses.
ASME specifications guarantee the safety and reliability of pressure components
but do not directly cut energy or consumable expenditure. To control operating
cost, the key lies in optimizing the compressed air system, implementing
preventive maintenance, minimizing gas leakage and matching equipment capacity
with actual gas demand. Refined operation management reduces production cost per
unit nitrogen, leverages the safety and stability advantages of ASME-compliant
equipment and achieves optimal full-lifecycle cost.