In many links of industrial production, nitrogen serves as an inert
protective gas with continuously expanding application scenarios. Industries
including chemical engineering, food preservation, pharmaceutical packaging and
laser cutting, as well as tank protection, all require continuous and stable
nitrogen supply. In the past, many enterprises commonly purchased bottled
nitrogen or liquid nitrogen to meet gas demands. Although simple to operate,
long-term use brings many pain points. Liquid nitrogen transportation requires
special cryogenic tank trucks and supporting cryogenic storage tanks, while
bottled nitrogen gas demands frequent replacement and handling. It not only
occupies site space, but is also affected by market prices and logistics
timeliness. Once gas supply is interrupted, production lines may shut down and
cause considerable economic losses. As enterprises’ demands for cost reduction
and efficiency improvement rise, on-site nitrogen generation solutions are
gaining popularity. With a simple structure and convenient operation and
maintenance, nitrogen generation equipment adopting membrane separation
technology has become a popular option in the commercial market.
Membrane commercial nitrogen generator achieves nitrogen-oxygen separation
based on the hollow fiber membrane separation principle. Clean compressed air
enters the membrane module. Gas molecules such as oxygen, water vapor and carbon
dioxide have faster permeation speed and pass through the membrane wall and get
discharged. Nitrogen molecules have low permeation rate and are trapped and
concentrated to produce nitrogen that meets process requirements. The whole set
of equipment does not require complex switching valves or adsorbent regeneration
processes. It starts to produce gas once powered on, featuring flexible start
and stop and fast response. It is well suited for commercial working conditions
requiring uninterrupted continuous gas supply.
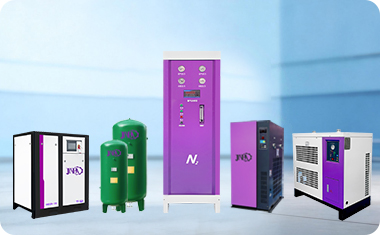
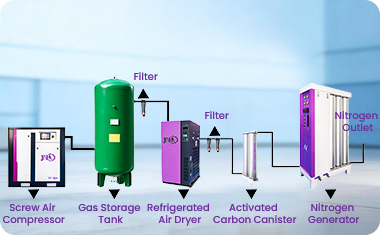
The whole system consists of an air compressor, air pretreatment unit,
membrane modules, buffer gas storage tank, control system, detection instruments
and other components. The air pretreatment unit is critical to extend the
service life of membrane modules. Oil stains, dust and moisture contained in
compressed air will damage hollow fiber membranes. Therefore, multi-stage
filtration and drying treatment are needed to remove impurities and guarantee
the cleanliness of air entering membrane elements. Purified compressed air is
sent into the membrane stack. Separated nitrogen is stored in the buffer tank to
stabilize pressure before delivery to each gas consumption point. Supporting
online detection devices monitor nitrogen purity in real time. Once parameters
deviate from the set range, the system will send out early warnings to help
operation and maintenance personnel troubleshoot in time.
Compared with pressure swing adsorption nitrogen generators, membrane
commercial nitrogen generation equipment has unique advantages. The equipment
features a compact structure, smaller overall size, less installation space
requirement, simple deployment and low capital investment. During operation,
there are no frequent valve switching actions, leading to low mechanical wear
and low operating noise. It has a low operation threshold and high automation
level, and can run 24 hours nonstop after startup without full-time on-site
operators. Routine maintenance is simple, mainly including regular filter
cartridge replacement. Membrane modules enjoy a long service life and can work
stably for a long time provided inlet air pretreatment reaches standards. For
commercial scenarios with stable gas consumption and medium nitrogen purity
requirements, the membrane separation nitrogen generation solution delivers
outstanding cost performance.
Nevertheless, it is necessary to objectively recognize its application
boundaries during model selection. Membrane separation nitrogen generation works
better for scenarios requiring medium and low nitrogen purity. If ultra-high
purity nitrogen is needed for production processes, other nitrogen generation
technologies should be evaluated. Meanwhile, inlet air pressure, inlet
temperature and air quality directly affect the flow rate and purity of produced
nitrogen. Excessively high inlet temperature or oil and moisture exceeding
standard in compressed air will accelerate aging of membrane elements and reduce
gas production efficiency. In the early stage of projects, enterprises need to
fully communicate with equipment suppliers combined with their own gas flow
demand, purity requirements and on-site environmental conditions, and customize
matched gas supply schemes to avoid waste caused by improper equipment
selection.
This type of equipment has a wide coverage of commercial application
scenarios. In the food processing industry, nitrogen is used for packaging
filling to isolate oxygen, slow down lipid oxidation and extend the shelf life
of snacks and beverages. In the chemical industry, it is applied for inert
protection at the top of storage tanks and pipeline purging to reduce safety
risks of flammable and explosive materials. In light industry and laser
processing, nitrogen acts as auxiliary gas to improve cutting surface quality
and prevent material oxidation under high temperature. Small and medium-sized
factories, storage bases and outdoor mobile operation stations can adopt such
equipment to build on-site gas supply systems and get rid of dependence on
externally purchased gas.
From the perspective of long-term operating costs, on-site membrane
nitrogen generation equipment has obvious advantages. After equipment
investment, it only consumes compressed air and a small amount of electricity.
Enterprises no longer bear large recurring expenses such as liquid nitrogen
procurement, cylinder rental and logistics transportation. Gas sources are
independently controllable and will not affect production due to gas market
price hikes or logistics delays. At the same time, it reduces operations related
to hazardous chemicals such as liquid nitrogen transportation and cylinder
transfer, lowers on-site safety management pressure and simplifies corporate gas
procurement processes.
Standard operation and maintenance are essential for any industrial
equipment to maintain stable performance for a long time. Daily inspections
should be carried out to track key parameters such as inlet pressure, nitrogen
purity and filter pressure difference. Filter cartridges need to be replaced on
schedule to prevent pollutants from entering membrane modules. Regular
inspection of pipeline joints is required to check for air leakage risks.
Standard protection measures should be taken if the equipment stops running for
a long period. Selecting suppliers with complete technical support and spare
parts supply capacity can reduce later operation and maintenance pressure.
The development of industry is also a process of continuous iteration and
upgrading of gas supply solutions. With a concise and reliable design, membrane
separation nitrogen generation technology provides a new on-site gas production
path for numerous commercial projects. When evaluating gas supply schemes,
enterprises should not only focus on equipment purchase price, but
comprehensively assess the full life-cycle cost, equipment stability and
maintenance difficulty. With proper model selection, standardized installation
and continuous maintenance, this on-site gas generation system can steadily
produce nitrogen, guarantee stable operation of production processes, help
enterprises cut costs and improve efficiency, and safeguard safe production.