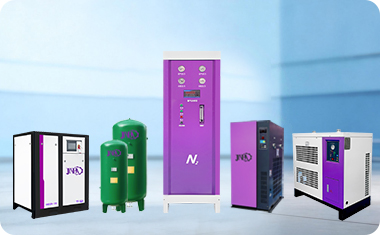
The PSA nitrogen generator system for lithium battery industry adopts
pressure swing adsorption as the core technology to produce high-purity nitrogen
on-site, widely used in lithium battery processes including electrode coating,
calendering, winding, liquid injection, formation, sealing and cell warehouse
storage. Lithium battery production is highly sensitive to water vapor and
oxygen. Cells exposed to oxygen compounds and high-humidity environments are
prone to side reactions, resulting in capacity fading, bulging and even thermal
runaway risks. The lithium battery PSA nitrogen generator system is not a
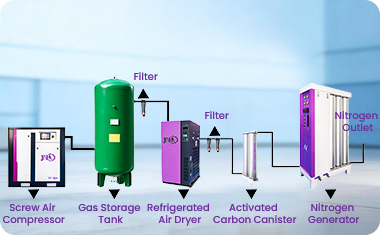
standalone nitrogen generation host, but an integrated complete system composed
of a pretreatment unit, PSA nitrogen adsorption host, buffer and pressure
stabilization unit, online monitoring unit, control interlock unit and exhaust
emission unit. All modules operate cooperatively to continuously supply
low-oxygen high-purity protective nitrogen to lithium battery workshops. From
air source purification, adsorption separation, pressure-stabilized delivery and
online monitoring to safety interlocking, it builds a complete inert gas supply
system to guarantee process stability and operational safety of lithium battery
production lines.
The air pretreatment subsystem serves as the first barrier of the whole
lithium battery PSA nitrogen generator system and directly protects the
downstream carbon molecular sieve adsorption medium. Water, oil mist and solid
dust contained in compressed air are major contaminants that degrade molecular
sieve performance. The pretreatment subsystem generally includes a refrigerated
dryer, multi-stage precision filters, activated carbon oil removal filters and
drainage assemblies. Compressed air output from the air compressor first enters
the refrigerated dryer to reduce the dew point of compressed air and remove most
free water. It then passes through precision filters of different accuracy
grades to filter solid particles and liquid oil droplets step by step. Activated
carbon filters deeply adsorb residual oil mist. Humidity inside lithium battery
workshops fluctuates greatly, so the pretreatment subsystem must steadily reduce
the dew point of inlet air and keep compressed air quality within design
specifications of the system. Once the pretreatment unit fails, water vapor and
oil contamination will flow directly into adsorption towers, contaminating
carbon molecular sieve and causing irreversible degradation of adsorption
capacity and shortening the service life of molecular sieve. Differential
pressure gauges are equipped in the pretreatment system to monitor filter
clogging status in real time. An early warning will trigger when differential
pressure exceeds limits, reminding maintenance staff to replace filter elements
promptly and prevent pollutants from breaking through into the downstream
nitrogen generation host.
The PSA adsorption nitrogen generation host subsystem is the core unit of
the gas supply system. It completes nitrogen-oxygen separation relying on the
selective adsorption characteristics of carbon molecular sieve. Inside the host
are two groups of adsorption towers filled with carbon molecular sieve
adsorbent. Under pressurized conditions, oxygen in air is adsorbed by molecular
sieve while nitrogen is enriched and exported. After adsorption saturation, the
tower depressurizes for regeneration to desorb adsorbed oxygen and complete
cyclic regeneration. The two adsorption towers alternately perform adsorption
and regeneration to realize continuous nitrogen output. To meet lithium battery
process requirements, the system adopts high-quality carbon molecular sieve to
maintain stable nitrogen purity under long-duration continuous working
conditions. The host is equipped with pneumatic valves, solenoid valves,
silencers and pressure sensors for adsorption towers. Valves switch
automatically according to preset time sequences to control the full cycle of
pressurization, adsorption, pressure relief and regeneration. Internal pressure
and temperature of the host are collected in real time and transmitted to the
central control system. Lithium battery production lines impose strict
requirements on nitrogen purity stability. Switching timing and operating
pressure of adsorption towers directly affect nitrogen purity. The control
system dynamically fine-tunes operating parameters according to load
fluctuations to stabilize nitrogen indicators and avoid purity fluctuations
interfering with cell manufacturing.
The buffer and pressure-stabilized delivery subsystem undertakes nitrogen
storage, pressure stabilization and distribution functions to ensure stable
nitrogen pressure delivered to lithium battery process equipment. This subsystem
consists of nitrogen buffer tanks, pressure regulating valves, pressure
transmitters, check valves, branch shut-off valves and pipe networks. Nitrogen
produced from the adsorption host first flows into buffer tanks, which buffer
pressure pulsation and reduce pressure fluctuations caused by alternate
switching of adsorption towers. Pressure regulating valves stabilize nitrogen
pressure to the process pressure required by lithium battery production lines.
Lithium battery workshops contain multiple production lines with different gas
pressure and flow requirements at different stations. The pressure-stabilized
delivery subsystem distributes nitrogen via branch pipelines to coaters, winding
machines, liquid injection cabinets and sealing equipment. Pressure monitoring
points are installed on pipelines to monitor pipe network pressure in real time.
Alarms will activate when pressure becomes excessively high or low. The whole
delivery pipeline network adopts clean pipelines with clean inner walls free of
oil contamination to prevent pipeline impurities entering cell stations and
contaminating products. Branch isolation valves are installed on pipelines. When
one production line needs maintenance, its gas supply can be cut off separately
without affecting nitrogen supply for other lines, improving operational
flexibility of the gas supply system.
The online monitoring and analysis subsystem monitors nitrogen quality and
system operating status in real time and acts as the perception module to
guarantee gas supply quality. This subsystem is equipped with online oxygen
analyzers, dew point detectors, flow sensors and pressure sensors. The oxygen
analyzer continuously detects oxygen concentration inside produced nitrogen, the
most critical monitoring indicator for lithium battery production. Excessive
oxygen content in nitrogen means failure of protective atmosphere, which
directly causes cell quality defects. Dew point meters monitor water content in
nitrogen and control water vapor indicators to prevent high water vapor entering
process chambers and inducing cell side reactions. All monitoring data is
uploaded in real time to the central control unit of the system and displayed
visually on the human-machine interface. Multi-level alarm thresholds are set in
the system. Level-1 early warnings indicate minor deviations and remind
maintenance personnel for inspection; level-2 high alarms trigger audible and
visual alerts and activate interlock protection actions when necessary.
Monitoring instruments must be calibrated regularly to prevent data distortion
caused by sensor drift, as false or missed alarms may bring quality risks to
lithium battery production. Monitoring data is automatically stored to form
production logs for process traceability, system audit and fault review.
The automatic control and safety interlock subsystem acts as the brain of
the lithium battery PSA nitrogen generator system and coordinates all units for
coordinated operation. Centered on a PLC with a human-machine touchscreen, the
control system collects all signals from pretreatment, adsorption host, buffer
pipe network and monitoring instruments, and automatically controls valve
timing, equipment startup/shutdown and alarm management. Operators can view
real-time operating parameters, historical curves and alarm records on the
touchscreen and switch equipment operating modes manually or automatically.
Safety interlock logic is the most important function of this subsystem with
multiple protection logics: low inlet pressure triggers early warning to prevent
gas supply interruption caused by air compressor failure; excessive oxygen
content in nitrogen triggers interlock alarm and cuts off delivery of
unqualified nitrogen to production lines when needed; system overpressure
triggers interlock pressure relief to protect storage tanks and adsorption
towers. Meanwhile, an emergency signal interface is integrated to connect with
the central control system of lithium battery workshops for remote monitoring
and remote shutdown. When abnormal working conditions occur, the system
automatically executes preset protective actions to reduce risks brought by
delayed manual response. The control system adopts hierarchical authority
management. Different maintenance personnel are assigned corresponding operation
permissions to prevent unauthorized personnel from modifying system parameters
arbitrarily and ensure safe system operation.
The tail gas emission and noise reduction subsystem handles oxygen-rich
tail gas discharged during regeneration, controls noise and optimizes workshop
operating environments. Oxygen-rich air released during adsorption tower
regeneration is discharged centrally through silencers and exhaust pipelines.
Silencers greatly reduce airflow noise generated by valve pressure relief and
gas exhaust to meet noise control standards of lithium battery workshops.
Exhaust pipelines are arranged away from densely manned operation zones.
Oxygen-rich air is directly discharged to outdoor atmosphere and will not
accumulate inside workshops. Lithium battery workshops contain large amounts of
organic solvents; oxygen-enriched environments raise combustion risks for
flammable solvent vapors. The design of tail gas pipelines fully considers wind
direction and diffusion conditions to prevent exhaust gas backflow into
workshops. Maintenance ports are installed on exhaust pipelines to facilitate
regular cleaning of dust and impurities inside pipes. No toxic or hazardous
substances are discharged from the whole emission system. This physical
separation process generates no waste liquid or chemical pollutants. Auxiliary
noise monitoring points continuously monitor noise at discharge outlets to
ensure workshop working environments meet occupational health standards.
The operation, maintenance and closed-loop management module guarantees
long-term stable operation of the whole nitrogen generation system. The system
has built-in maintenance reminder functions that automatically push maintenance
alerts according to equipment running time, filter differential pressure and
molecular sieve operating duration. Maintenance staff carry out regular
inspections to verify instrument, valve and pipeline status of each subsystem,
replace filter elements periodically and check molecular sieve performance.
Energy isolation, pressure relief and lockout-tagout procedures are implemented
during maintenance operations to guarantee overhaul safety. Maintenance records
are entered into the system database to build a full-lifecycle maintenance
archive. The system has built-in fault diagnosis functions. When valve
abnormality, loss of instrument signals or abnormal pressure occurs, it
automatically locates fault positions to help maintenance personnel troubleshoot
rapidly. Nitrogen generation systems in lithium battery factories often adopt a
parallel multi-unit structure. Multiple nitrogen generators serve as mutual
backups. When one unit shuts down due to faults, the standby unit automatically
starts to guarantee uninterrupted gas supply for production lines and avoid
production line stoppage and cell scrap caused by gas source interruption.
To sum up, the PSA nitrogen generator system for lithium batteries is a
complete industrial gas supply system with multi-unit coordination, online
monitoring and safety interlock capabilities. From air pretreatment, PSA
nitrogen adsorption host, buffer delivery, online monitoring and PLC interlock
control to tail gas emission, all subsystems cooperate closely and none is
dispensable. Lithium battery manufacturing is extremely sensitive to oxygen and
water. This system continuously supplies low-oxygen, low-dew-point high-purity
nitrogen to provide inert protective atmosphere for key processes such as
coating, winding, liquid injection and sealing. The system can not only steadily
guarantee the quality of process gas, but also identify hidden faults in advance
through multi-stage monitoring and interlock protection, reducing production
risks such as batch cell defects and thermal runaway. Constructing a complete
PSA nitrogen generator system together with standardized maintenance schemes in
lithium battery factories can continuously and stably supply protective
nitrogen, replace purchased high-pressure nitrogen cylinders, lower safety risks
and overall costs from cylinder transportation and replacement, and support
long-term stable and safe production of lithium battery lines.