In the modern industrial system, nitrogen is one of the most widely used
and largest-volume industrial gases. From steel metallurgy, glass manufacturing,
and chemical production to electronic components, pharmaceutical ingredients,
and food packaging, almost every type of large-scale manufacturing activity
relies on nitrogen. As industry upgrades and production lines expand, the demand
for nitrogen keeps rising, and requirements for supply stability, purity, and
cost become increasingly stringent. Whether enterprises can meet industrial gas
needs economically, stably, and in the long term has become a core concern for
many manufacturers.
For a long time, the main sources of nitrogen for industrial enterprises
were purchased liquid nitrogen and bottled gas. Liquid nitrogen requires
cryogenic storage tanks and dedicated tanker transportation, while cylinders
depend on frequent replacement and centralized management. Although both methods
are mature, they face practical problems such as high transportation costs,
dependence on the external supply chain, and numerous management steps. Once
logistics are delayed or supply is tight, production rhythm is often directly
affected. To break out of this passive situation, more and more factories are
turning to on-site nitrogen generation, establishing generation units on site to
achieve self-supply and reduce dependence on external sources.
Among the many on-site nitrogen production technologies, membrane
separation has gained wide application in industry thanks to its own strengths.
Such industrial membrane separation nitrogen production units use the difference
in permeation rates of different gas molecules through hollow fiber membranes to
achieve gas separation. Clean compressed air enters the membrane module, and
molecules that permeate faster, such as oxygen and water vapor, pass through the
membrane wall first and are discharged, while slower-permeating nitrogen is
enriched and retained, continuously producing nitrogen that meets process
requirements. The whole system has no complex switching valves and no periodic
adsorbent regeneration process. It starts producing gas as soon as it is powered
on, starts and stops flexibly, and matches the continuous, stable gas demand of
industrial sites.
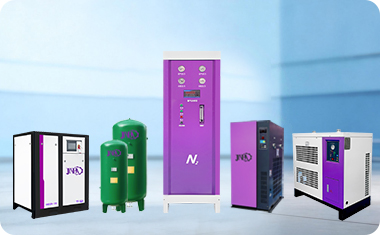
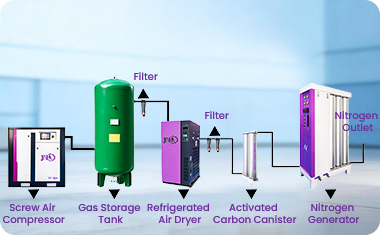
A complete industrial-grade membrane separation nitrogen system usually
consists of an air compressor, an air pretreatment unit, membrane modules, a
buffer storage tank, and control and detection systems. Among these, the air
pretreatment unit is especially critical. Compressed air on industrial sites
often contains oil, water, and dust. If these impurities are not removed, they
significantly shorten the life of hollow fiber membranes and reduce purity and
flow. Therefore, before entering the membrane module, air must undergo
multi-stage filtration and drying to ensure it is clean, dry, and at stable
pressure. The separated nitrogen enters the buffer storage tank to stabilize
pressure and is then delivered on demand to each point of use.
When choosing nitrogen production technology, industrial users often
compare membrane separation with pressure swing adsorption. Membrane separation
equipment is compact, starts up quickly, requires no frequent switching or
regeneration process, and offers a high degree of automation and reliable
long-term operation, suiting scenarios with large and continuously stable gas
demand. Pressure swing adsorption is better at producing high-purity nitrogen
and suits processes with strict purity requirements. The two have their own
applicable boundaries. Enterprises need to choose the solution that best fits
their process based on specific requirements for purity, flow, energy
consumption, and maintenance cost, and may combine approaches when
necessary.
Industrial gas usage conditions are complex and variable, which places
higher demands on the reliability of nitrogen systems. Equipment must operate
stably for long periods in environments with high temperature, dust, and
vibration, so weatherability, sealing, and the robustness of control systems are
all crucial. At the same time, online purity monitoring and fault alarms are
indispensable. For high-value processes, oxygen analyzers feed back gas purity
in real time. Once values deviate from the set range, the system immediately
alarms and switches over to prevent unqualified nitrogen from entering the
production line. Complete localized services and spare-part supply are important
conditions for ensuring stable long-term operation.
Industrial membrane nitrogen production equipment has wide application. In
the food and beverage industry, it is used for nitrogen-filled packaging and
tank inerting to exclude oxygen and extend shelf life. In the chemical industry,
it participates in tank blanketing, pipeline purging, and protection of
flammable materials. In laser cutting and metal processing, nitrogen acts as an
auxiliary gas to improve cutting quality and prevent high-temperature oxidation.
In electronics manufacturing, high-purity nitrogen is used to create oxygen-free
environments and protect sensitive materials. From large factories to
distributed gas stations, membrane separation nitrogen production helps
enterprises build self-controlled gas source systems.
From a cost perspective, the economic value of on-site industrial nitrogen
generation is equally prominent. Although equipment requires an initial
investment, over its entire life cycle the operating cost mainly consists of
compressed air and electricity, far lower than the long-term cost of
continuously purchasing liquid nitrogen, and is not easily affected by gas
market price fluctuations. More importantly, on-site generation reduces the
links of hazardous chemical transportation, storage, and loading, lowering
safety risks and compliance burdens and making gas management more centralized
and transparent. For enterprises with large gas demand, this usually brings
considerable return on investment in the long run.
Any industrial equipment needs scientific operation and maintenance to
deliver lasting value. Daily maintenance should track key parameters such as
inlet pressure, gas purity, and filter pressure difference, replace filter
cartridges on time to prevent pollutants from damaging membrane elements,
regularly inspect pipelines and joints to eliminate air leakage risks, and
protect the equipment according to specifications during long shutdowns. At the
same time, enterprises should choose suppliers with mature technology and
complete after-sales support so that the equipment receives timely, professional
care throughout its life cycle.
It is foreseeable that, as membrane materials and nitrogen production
processes continue to advance, the performance of industrial membrane nitrogen
generation technology will keep improving, with purity, energy consumption, and
intelligence all being optimized, and it will play an increasingly important
role in more industrial scenarios. For enterprises, scientifically assessing gas
demand, choosing the right nitrogen production technology and supplier,
installing in a standardized way, and maintaining continuously are what truly
allow on-site nitrogen generation to safeguard production and provide solid
support for high-quality development.