The outdoor industrial nitrogen generator is an integrated, containerized
on-site gas production device. It adopts Pressure Swing Adsorption (PSA)
technology to separate nitrogen directly from ambient air at open-air and remote
construction sites without constructing dedicated workshops. The equipment
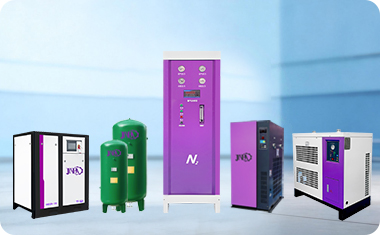
integrates an air compressor, drying and purification units, filter assemblies,
nitrogen generation host, buffer gas storage tank and intelligent control system
inside a reinforced container enclosure. It has outdoor protection against rain,
dust and temperature fluctuations, suitable for oil & gas, mining, field
engineering and temporary construction sites without enclosed workshops. It
replaces traditional nitrogen cylinder or liquid nitrogen supply solutions and
enables continuous on-site gas supply.
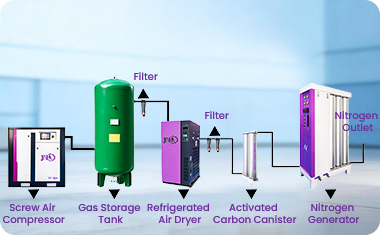
The core principle of outdoor industrial nitrogen generators is pressure
swing adsorption. Ambient air is compressed by an air compressor and sent to a
pretreatment system. Multi-stage filters and refrigerated dryers remove oil,
dust and moisture from compressed air. Purified dry compressed air flows into
adsorption towers filled with carbon molecular sieves. Carbon molecular sieves
selectively adsorb oxygen molecules. Under pressurization, oxygen in air is
adsorbed while nitrogen molecules pass through the sieve and are enriched. Once
adsorption saturation is reached, the system switches towers automatically.
Pressure reduction desorbs and discharges trapped oxygen to regenerate molecular
sieves. Two adsorption towers cycle alternately between adsorption and
regeneration to steadily produce nitrogen continuously. Nitrogen purity
typically ranges from 95% to 99.999% and can be adjusted online according to
process requirements. The whole separation process runs at ambient temperature
without chemical reactions, delivering safe operation and stable energy
consumption.
Operating outdoors involves harsh environments, so housing and structural
design are critical. The container shell features anti-corrosion coating and
waterproof sealing. Ventilation louvers and rainproof sun canopies are installed
to resist rain, dust and day-night temperature variation. Internal electrical
components are wide-temperature rated to operate stably under high and low
temperatures. Pipes and valves adopt corrosion-resistant materials to reduce
aging and rust in humid field environments. Inspection doors are reserved for
on-site inspection, filter and molecular sieve replacement. Lifting bases
support whole-unit transportation. After project completion, the unit can be
hoisted and towed to the next site for reuse. Fully assembled, pressure-tested
and pre-commissioned before delivery, the unit only requires a hardened
foundation, power supply and output pipeline connection for rapid commissioning
on site.
The unit is equipped with an intelligent monitoring system that tracks
nitrogen purity, outlet pressure, flow rate, tower pressure and internal cabinet
temperature and humidity in real time. An inline oxygen analyzer continuously
measures product gas purity. If purity falls below the set threshold, the system
triggers automatic alarms and interlock protection. The touchscreen HMI displays
operating parameters and supports remote data transmission. Operators can
remotely monitor working conditions and log operation records. Built-in fault
diagnostics automatically warn of clogged filters, abnormal pressure and valve
faults to reduce shutdown risks during unattended field operation.
Outdoor industrial nitrogen generators are widely used in oil and gas
pipeline purging, tank blanketing, underground mine fire suppression, field
welding shielding and pipeline pressure test protection. Compared with
purchasing liquid nitrogen or cylinder gas, it eliminates gas transportation,
filling, cylinder handling and return refilling, greatly cutting long-term gas
supply costs and removing safety hazards caused by cylinder transport and
cryogenic liquid nitrogen handling. For remote field projects with long
transport distances and difficult gas resupply, on-site nitrogen production
delivers outstanding advantages.
Long-term stable operation relies on regular preventive maintenance.
Routine inspections focus on cabinet sealing, filter pressure differential,
compressor lubricant and pipeline air tightness of adsorption towers. Failed
filters must be replaced promptly to prevent oil and water from contaminating
molecular sieves and deactivating adsorbent materials. During rainy seasons,
cabinet drain holes need inspection to avoid water accumulation. Anti-freezing
insulation is required in cold winter conditions. Carbon molecular sieves have
limited service life and degrade gradually over runtime and need inspection and
replacement at end-of-life. The cabinet should remain sealed during storage to
prevent dust and rain ingress.
Outdoor industrial nitrogen generators simplify nitrogen supply for field
industrial work. By packing air separation equipment into mobile containers,
they adapt to variable open-air environments and guarantee stable nitrogen
supply for field projects. Proper equipment selection and standardized
maintenance can deliver consistent shielding gas and provide reliable,
economical on-site gas solutions for outdoor industrial operations.