As an integrated and mobile all-weather industrial nitrogen production
solution, containerized nitrogen generators are widely used in field
engineering, oil and gas exploitation, mining operations, temporary factory
areas, remote projects and other gas supply scenarios without fixed equipment
rooms. Different from traditional fixed nitrogen production equipment, it
features integrated container cabinet, installation-free foundation, movable
transportation and all-weather outdoor operation, forming a diversified
quotation system. The market price of containerized nitrogen generators varies
greatly, ranging from hundreds of thousands of yuan for small and medium-sized
standard models to millions of yuan for large customized explosion-proof models.
The price difference is not simply determined by equipment specifications, but
jointly affected by six core dimensions: configuration standard, performance
parameters, customized requirements, material technology, brand service and
long-term operating cost. In procurement and selection, enterprises should not
only focus on the initial quotation, but judge the cost performance based on
comprehensive value to avoid procurement misunderstandings of low price with
poor quality and redundant high-cost configuration.
Basic equipment parameters constitute the core benchmark for containerized
nitrogen generator pricing. Gas production flow rate and nitrogen purity are two
key pricing indicators, following the industry rule that larger flow rate and
higher purity lead to higher unit price. Standard medium and small-flow
container nitrogen generators with low purity of 95%–99% have simple structures
and conventional core configurations with relatively low procurement cost,
suitable for ordinary purging, protection and basic process gas supply. In
contrast, high-purity models with nitrogen purity of 99.9%–99.999% require
high-density high-quality carbon molecular sieves, high-precision detection
systems and multi-stage deep purification devices, which greatly increase the
cost of core separation and measurement components. Besides, rated working
pressure, continuous operation load and start-stop accuracy also affect the
selection of core accessories and further widen the price gap between different
models.
Cabinet material, process standard and outdoor adaptive configuration are
exclusive pricing variables that distinguish containerized models from fixed
nitrogen generators. Containerized equipment needs to adapt to complex outdoor
working conditions such as open-air exposure, extreme temperature, wind and
sand, humidity and corrosion, requiring strict cabinet structure and protection
technology. Low-cost models mostly adopt ordinary carbon steel cabinets with low
protection level and simple anti-corrosion technology, only suitable for
temporary indoor or sheltered environments. Mid-to-high-end models adopt
thickened anti-corrosion carbon steel or 304 stainless steel structures with
sandblasting, multi-layer anti-corrosion spraying and integral waterproof
sealing, reaching IP54 or higher protection level. They can withstand extreme
temperatures from -40℃ to 60℃ and support all-weather outdoor operation.
Auxiliary configurations such as constant temperature insulation system, rain
and dust prevention structure and ventilation heat dissipation device also
increase production cost and cause price differences.
Customized functions and special working condition configurations are the
main reasons for the price increase of high-end models. Standard general models
have transparent prices and stable cost performance, while customized
modifications for special industries greatly improve equipment value and
quotation. Equipment applied in oil, gas and chemical flammable and explosive
scenarios needs complete explosion-proof systems, explosion-proof electric
control cabinets, solenoid valves and lightning and static protection devices.
Food and pharmaceutical industry models are equipped with sterile stainless
steel pipelines, oil-free purification systems and sanitary-grade filtration
configurations. Unattended field projects require remote wireless monitoring,
cloud data transmission, automatic fault early warning and intelligent
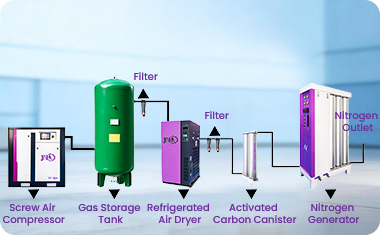
energy-saving control systems. Meanwhile, the integrated all-in-one design with
built-in air compressor, refrigerated dryer and gas storage tank requires no
external supporting equipment, featuring higher integration level, higher
assembly cost and higher price than split models.
Core accessory supply chain and production processes directly determine
equipment quality and pricing range. Low-cost models adopt low-end ordinary
molecular sieves, universal solenoid valves and simple control systems,
featuring poor durability, high energy consumption and high failure rate with
high later maintenance costs. High-end brand models adopt long-life high-purity
carbon molecular sieves, first-class brand pneumatic components, high-precision
sensors and intelligent PLC control systems, ensuring strong stability, low loss
and long service life. In addition, refined pipeline layout, standardized
welding technology and strict factory inspection increase working hours and
quality control costs, but effectively ensure long-term stable operation and
reduce shutdown risks, realizing long-term cost-effective investment.