The fully automatic PSA nitrogen generator is a professional gas production
equipment developed based on mature oxygen-nitrogen separation principles and
modern industrial automatic architecture. Optimized in five core design
dimensions including system structure, core technology, automatic control logic,
protective structure and operation maintenance adaptation, it abandons the
shortcomings of traditional nitrogen making equipment such as redundant
structure, high energy consumption, unstable purity and complicated operation.
Adopting integrated modular design and intelligent cycle technology, it realizes
unattended and continuous stable gas production, perfectly meeting the
high-purity nitrogen demand of new energy lithium battery, electronic
manufacturing, food preservation, precision hardware, chemical explosion-proof
and other industries, serving as a standardized preferred equipment for on-site
industrial nitrogen supply.
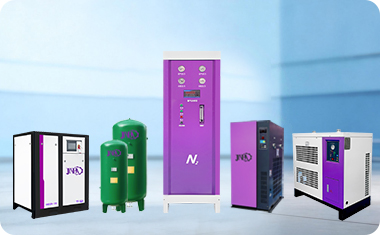
In terms of overall structural design, the equipment adopts an integrated
modular structure following the industrial design principles of compact layout,
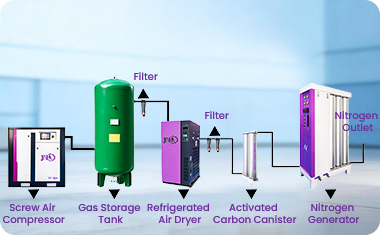
efficient heat dissipation and space saving. It highly integrates the air
pretreatment unit, PSA separation core unit, intelligent control unit and
pressure stabilization gas storage unit on an integral base, eliminating the
problems of messy pipelines, cumbersome installation and large floor area of
traditional split equipment. The optimized air duct and heat dissipation
structure with a special airflow diffusion device effectively avoids molecular
sieve pulverization and airflow disorder caused by high-speed airflow impact,
smoothes the internal gas circulation, and greatly improves the overall
operational stability to adapt to workshops with limited installation space.
Equipped with a mature dual-tower PSA cycle separation technology and an
upgraded 9-valve unequal pressure equalization system, the equipment features
outstanding high efficiency and energy saving. Taking compressed air as raw
material, it realizes precise oxygen-nitrogen separation by utilizing the
different adsorption rates of carbon molecular sieves for oxygen and nitrogen
through pressure adsorption and pressure relief desorption. The two adsorption
towers alternately complete the whole process of adsorption and gas production,
pressure relief regeneration, pressure equalization energy storage and flushing
reset. Compared with traditional 8-valve models, it efficiently recovers
residual pressure and nitrogen energy in the tower, greatly improves energy
utilization rate, and reduces overall energy consumption and standby gas
consumption. Equipped with high-precision carbon molecular sieves, it stably
outputs high-purity nitrogen with adjustable purity ranging from 95% to 99.9995%
to meet diverse working condition standards.
As the core intelligent configuration, the customized PLC automatic control
system supports full-process unmanned operation. After startup, the equipment
automatically completes air filtration, pressure regulation, tower switching,
molecular sieve regeneration and stabilized nitrogen output. The system
adaptively adjusts adsorption and regeneration cycle parameters according to
real-time gas consumption fluctuations, solving the problems of unstable purity
and energy waste caused by peak and valley gas consumption. Built-in intelligent
monitoring modules real-timely detect core data such as nitrogen purity, working
pressure and operating temperature, with functions of overload, overpressure,
self-inspection, fault alarm and emergency stop protection, avoiding equipment
loss caused by idling and overload operation and ensuring long-term stable
operation.
Optimized for complex industrial working conditions, the equipment realizes
excellent durability and anti-interference performance. The thickened
pressure-bearing tower with patented internal balance compression structure and
professional molecular sieve filling technology prevents molecular sieve
loosening and pulverization, extending the service life of molecular sieves and
reducing maintenance frequency. Industrial-grade wear-resistant and
anti-corrosion pipelines and valves adapt to long-term high-frequency start-stop
and high-pressure cycle operation. The front-end multi-stage precision
pretreatment system removes moisture, oil and dust impurities from compressed
air, preventing molecular sieve contamination and failure, and laying a solid
foundation for long-term stable operation.
Focusing on convenient later maintenance, the modular partition layout and
standardized pipeline interface simplify disassembly, inspection and parts
replacement, greatly reducing operation difficulty and maintenance costs. The
fully automatic operation eliminates manual duty and labor costs, while the
energy-saving process reduces long-term operating energy consumption. With
comprehensive design optimization in structure, technology, automatic control,
protection and maintenance, the fully automatic PSA nitrogen generator
integrates stability, energy efficiency, practicality and economy, fully
satisfying the high-efficiency, low-carbon and intelligent on-site gas
production needs of modern industries.