With the continuous upgrading of global food safety standards and consumer
demands for food quality, fresh taste, and long shelf life, modern food
packaging industries are abandoning traditional packaging methods that cause
oxidation, moisture deterioration, and bacterial growth. A professional nitrogen
compressor for food packaging has become an essential core device for modified
atmosphere packaging (MAP), widely used in packaging of puffed snacks, nuts,
bakery products, pre-cooked meals, and meat products. It delivers clean, stable,
oil-free nitrogen supply to maximize food freshness, extend shelf life, and
reduce production waste for food manufacturers.
Nitrogen is an inert, safe, and non-toxic gas that does not react with food
ingredients or support microbial reproduction, making it the ideal gas for food
preservation. However, high-quality nitrogen packaging results rely entirely on
reliable nitrogen compression equipment. Ordinary industrial compressors cannot
meet food-grade standards due to oil contamination, unstable pressure, impure
gas output, and inconsistent airflow, which easily cause food pollution, uneven
nitrogen filling, packaging collapse, and high defective rates. Tailored for the
food and beverage industry, the professional nitrogen compressor for food
packaging strictly complies with food-grade hygiene regulations, solving all
pain points of traditional packaging equipment and supporting standardized,
automated food packaging production.
The food packaging nitrogen compressor features four core advantages:
oil-free clean output, precise pressure control, high energy efficiency, and
wide application compatibility. Adopting a full oil-free compression structure
and sanitary stainless steel pipelines, the equipment completely avoids
lubricant leakage, ensuring zero oil, zero water, and zero impurities in
nitrogen output. It fully meets global food safety compliance requirements and
eliminates secondary pollution to packaged food, which is critical for high-end
and export food production.
This nitrogen compressor supports adjustable stable working pressure from
0.1MPa to 0.5MPa, perfectly matching the nitrogen filling demands of diverse
food categories. For crispy puffed snacks and biscuits, stable nitrogen pressure
removes oxygen inside packaging bags and forms a protective cushion to prevent
extrusion damage during transportation and storage, preserving original crisp
taste. For high-fat nuts and dried fruits, high-purity nitrogen isolated oxygen
effectively delays fat oxidation and rancidity, greatly extending product shelf
life. For pre-cooked dishes and fresh meat products, nitrogen atmosphere
packaging inhibits harmful bacteria growth, enabling safe and long-term
preservation without excessive preservatives, meeting the healthy consumption
trend.
Designed with compact structure, low vibration, and low noise, the nitrogen
compressor for food packaging can be seamlessly integrated with fully automatic
packaging production lines without factory reconstruction, adapting to small
workshops and large-scale food factories alike. Equipped with an intelligent
control system, the device supports 24-hour continuous stable operation with
fast start-stop response and uniform gas flow, effectively reducing defective
packaging rates caused by unstable air supply and significantly improving
production efficiency.
In terms of operational cost, this energy-efficient nitrogen compression
equipment greatly reduces daily power consumption. Compared with purchasing
bottled nitrogen, the on-site nitrogen compression system cuts more than 30% of
packaging gas costs for food enterprises. Featuring corrosion-resistant and
aging-resistant materials, the compressor adapts to humid and dusty food
production environments, with stable operation, low failure rate, and simple
daily maintenance, minimizing downtime losses and later maintenance costs.
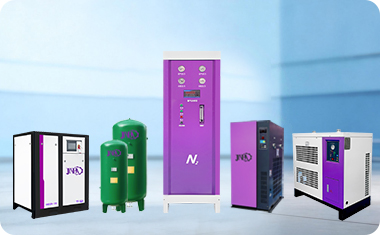
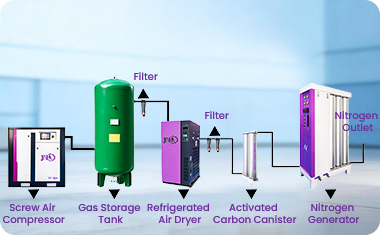
Moreover, the food-grade nitrogen compressor can work perfectly with
nitrogen generators to realize integrated nitrogen production, compression, and
filling. It maintains stable nitrogen purity above 99%, meeting different food
preservation grade requirements. As modified atmosphere packaging becomes the
mainstream of the food packaging industry, professional nitrogen compressors
have become indispensable supporting equipment for food quality improvement,
safety compliance, and cost reduction.
In conclusion, the high-performance nitrogen compressor for food packaging
empowers food manufacturers to upgrade packaging technology, ensure food safety,
reduce product loss, and enhance market competitiveness. It is the most reliable
and cost-effective solution for modern food fresh-keeping packaging
production.