Comprehensive cost evaluation of small business nitrogen generators is the
primary core consideration for small and medium industrial enterprises
undertaking on-site inert gas source transformation projects. Many small
processing factories, food packaging workshops, laser processing workshops and
auxiliary workshops for minor chemical processes rely on purchased high-pressure
nitrogen cylinders for a long time, continuously bearing hidden expenses such as
cylinder rental fees, transportation charges, deposits and labor cost for
cylinder replacement. A small business nitrogen generator is not merely the
purchase price of equipment; it represents the total cost of ownership (TCO)
covering initial investment, installation support, annual operation &
maintenance, energy consumption loss, spare part replacement and downtime
losses. For small enterprises with limited scale and tight budgets, only
comparing equipment quotation is insufficient. Based on industrial application
scenarios, companies need to fully calculate investment, payback period and
long-term risks, judge whether the on-site nitrogen generation scheme matches
the gas demand of their own production lines, and realize cost reduction and
efficiency improvement for gas supply in industrial production.
Initial capital investment is the most intuitive one-time expenditure of a
small business nitrogen generator project, and also the top concern for small
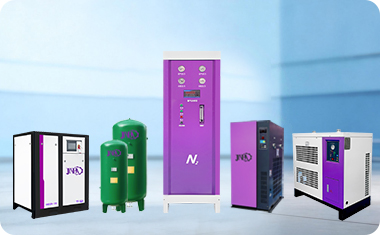
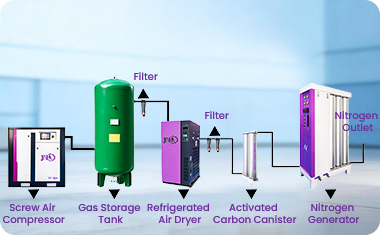
and medium enterprises. The complete system includes PSA nitrogen generation
host, air pretreatment unit, air compressor, buffer gas storage tank, pressure
regulating pipeline, PLC control system and online monitoring instruments.
Equipment purchase price is mainly affected by gas output, nitrogen purity,
outlet pressure and skid-mounted integration level. Higher purity and larger
flow rate raise the specifications of the main unit, filling volume of carbon
molecular sieve and standard of filter configuration, pushing up procurement
cost synchronously. Basic models only satisfy fundamental gas supply
requirements. Optional accessories such as high-purity analytical instruments,
remote monitoring modules, redundant standby units and explosion-proof
electrical appliances will increase upfront investment. Apart from the main
equipment cost, there are auxiliary engineering expenses: workshop site
renovation, ventilation pipeline laying, electrical wiring, air tightness
pressure testing, instrument calibration and hoisting positioning for
installation and construction. Some workshops also require floor reinforcement
and noise reduction protection. These auxiliary engineering items are often
overlooked by small businesses and result in budget overruns.
In industrial project accounting, matching selection directly determines
investment effectiveness. Many small businesses cut budgets by purchasing
undersized nitrogen generators. During peak production periods, insufficient gas
supply reduces nitrogen purity and harms product yield. Others blindly purchase
oversized models; equipment runs under no-load conditions for a long time,
raising energy consumption per unit gas production and extending the payback
period. The core principle for model selection in industrial scenarios is to
superimpose peak margin based on average daily gas consumption, match the
maximum instantaneous gas demand of production lines and take purity indicators
into account. Different processes such as food preservation and laser protection
have significantly different requirements for nitrogen purity. Basic models with
99.5% purity cost less, while scenarios like lithium battery supporting and fine
chemical industry require high-purity nitrogen above 99.99%, and equipment cost
rises obviously. Before model selection, enterprises collect actual gas
consumption data over 3 to 6 months, calculate the average hourly gas
consumption, and carry out load simulation by equipment manufacturers to avoid
unnecessary capital waste caused by improper selection.
Operating energy consumption is the variable recurring cost of a small
business nitrogen generator and accounts for the largest proportion in the
full-lifecycle cost. Energy consumption of the whole system mainly comes from
air compressors, followed by dryers, control systems and monitoring instruments.
The nitrogen generator itself only completes adsorption separation and consumes
almost no electric power. The energy efficiency grade and running time of air
compressors directly decide the power consumption cost per cubic meter of
nitrogen. Electricity price is a key external variable affecting energy
expenses. Differences in industrial electricity prices across regions will
significantly change annual operating expenditure. In continuously operated
industrial workshops, equipment runs all year round and electricity bills accrue
steadily each month. Intermittent production enterprises start equipment only
during production shifts, and energy consumption cost reduces accordingly.
Methods to optimize energy consumption include selecting high-efficiency air
compressors, optimizing air pretreatment to reduce pipeline resistance and
checking pipeline leakage regularly. Tiny pipeline air leakage seems trivial,
but long-term accumulation increases compressor loading time and power
consumption. Industrial practice proves that supporting high-quality
pretreatment systems to reduce oil, dust contamination of molecular sieve and
maintain efficient equipment operating conditions can continuously cut energy
consumption per unit gas output and reduce monthly electricity bills.
Preventive operation & maintenance and spare parts costs are periodic
fixed expenditures, often underestimated by small and medium enterprises in the
early project stage. Consumables include multi-stage air filter elements,
desiccants and solenoid valve seals. Carbon molecular sieve needs replacement
after long-term operation. Filter elements are high-frequency replacement parts;
they are generally replaced quarterly or semi-annually depending on dust and oil
mist in workshops. Replacement cycles for desiccants and valve seals are longer,
mostly annual maintenance items. As the core adsorption medium, carbon molecular
sieve can work for many years under well-maintained working conditions. However,
if inlet air purification fails, molecular sieve will quickly pulverize and
fail, requiring overall replacement as a major spare part expense. Maintenance
costs also include annual on-site inspection, instrument calibration and manual
service fees for system linkage testing. Enterprises with in-house maintenance
staff can finish basic inspection and filter replacement independently to reduce
outsourced maintenance service fees. Small factories lacking professional
personnel need to sign annual maintenance contracts, raising O&M budgets.
Ignoring regular maintenance leads to equipment performance degradation,
declining nitrogen purity and even unexpected shutdown, causing greater
production losses.
Downtime and production risk costs are hidden costs easily ignored in
industrial cost calculation. Small enterprises have limited production scale and
little fault tolerance space. Once nitrogen generation equipment breaks down and
the on-site inert protective gas supply is interrupted, downstream processes
shut down directly. Without nitrogen protection in food packaging, metal heat
treatment and laser welding processes, products oxidize and develop surface
defects, scrapping whole batches of materials. Downtime cost includes labor loss
during shutdown, compensation for delayed orders and raw material scrap loss. To
mitigate such risks, industrial project schemes may add buffer gas storage tanks
to maintain short-time gas supply relying on nitrogen stored in tanks during
brief equipment maintenance. For key production lines requiring uninterrupted
gas supply, a small standby nitrogen generator unit can be equipped. Although
initial investment rises, economic losses caused by shutdown are greatly
reduced. When enterprises evaluate costs, potential losses from equipment
downtime should be incorporated into calculation to comprehensively compare
long-term benefits of basic single-unit models and schemes with standby
redundancy.
A comparison with traditional cylinder gas supply can intuitively reflect
the economy of small business nitrogen generators. When purchasing bottled
nitrogen, expenses include gas unit price, cylinder rental, transportation and
delivery fees, cylinder deposit and labor cost for cylinder replacement. Bottled
nitrogen carries high unit price together with supply chain risks. Delivery
delays or gas source shortages directly shut down production lines. After
one-time investment in on-site nitrogen generation equipment, enterprises only
bear electricity bills and consumable spare part fees afterwards, and gas
production cost per unit is far lower than bottled nitrogen. Under stable and
continuous gas consumption in most small and medium industrial scenarios, the
equipment payback period is generally 1 to 2 years. If factories experience
volatile gas usage, intermittent production and low monthly gas consumption,
equipment utilization will be insufficient, extending the payback period
significantly, and even making cylinder purchase more economical. Therefore,
small enterprises must calculate based on their own gas consumption scale
instead of relying solely on marketing promotion when evaluating costs, and
judge whether the payback period meets business expectations.
At the financial and project support level, some indirect cost factors
affect overall investment. Plant floor occupation cost: skid-mounted nitrogen
generator sets require independent workshop placement zones with reserved space
for maintenance and ventilation, occupying workshop area. Noise cost: noise
generated by air compressors and valve switching requires noise reduction
cabinets and vibration damping bases if workshops are close to office areas,
generating renovation expenses. In addition, equipment depreciation, insurance,
annual safety inspection and compliance verification also count as long-term
costs. In industrial project investment calculation, these costs are allocated
by equipment depreciation years and counted into annual expenses. Some regions
offer technical transformation subsidies and special energy-saving support
policies for industrial equipment. Eligible small and medium enterprises can
apply for subsidies to reduce initial capital investment and shorten the payback
period. Finance departments of enterprises can treat the equipment as fixed
assets for depreciation to optimize tax costs and further improve the overall
economy of the project.
To sum up, evaluating the cost of a small business nitrogen generator must
adopt the industrial mindset of full-lifecycle cost analysis rather than only
checking equipment quotation. Initial procurement, installation support,
electricity energy consumption, periodic spare part maintenance and potential
downtime losses together form a complete cost system. For small and medium
industrial enterprises, proper equipment matching is the key to cost control.
Select appropriate specifications according to actual gas flow, purity demand
and workshop working conditions to avoid oversized units with low load or
insufficient gas supply capacity. Stable gas demand is the prerequisite for
on-site nitrogen generation schemes to exert cost advantages. Food, laser
processing and minor heat treatment workshops with steady continuous gas
consumption can usually recover investment within a short cycle. Enterprises
with scattered gas usage and low monthly gas consumption need careful
assessment. From the perspective of long-term industrial production operation,
properly selected equipment together with standardized maintenance enables small
business nitrogen generators to replace traditional bottled nitrogen, eliminate
safety hazards from cylinder transportation, replacement and storage,
continuously reduce comprehensive cost of inert protective gas supply for
industrial production and stably guarantee process quality of production lines.
Before project approval, enterprises should fully collect gas consumption data,
calculate total cost of ownership, assess return on investment and make gas
source transformation decisions matching their production budgets.