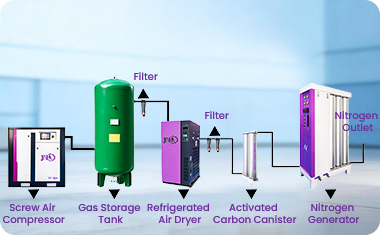
Membrane separation nitrogen generators have become core supporting equipment in the modern food preservation industry by virtue of their energy efficiency, stability, low maintenance and adjustable purity characteristics. Based on hollow fiber membrane separation technology, the equipment uses the different permeation rates of oxygen, nitrogen and other gas molecules in compressed air to realize physical separation without chemical reaction. Oxygen, water vapor and other impurity gases penetrate the membrane fiber rapidly and are discharged, while high-purity nitrogen is retained and output stably. The nitrogen purity produced by membrane separation equipment can be flexibly adjusted between 90% and 99.5%, which is more in line with the graded preservation needs of different food products than single-purity nitrogen equipment, and perfectly adapts to the modified atmosphere packaging (MAP) and controlled atmosphere storage requirements of the food industry.
In food preservation applications, the core value of membrane separation nitrogen generators is to inhibit food oxidation and microbial growth to extend shelf life. Oxygen is the main cause of food deterioration, which will lead to fat oxidation, color fading, flavor loss and mass propagation of aerobic bacteria and molds. By filling high-purity nitrogen into food packaging bags, storage containers and warehouses, the equipment can effectively displace internal air, reduce oxygen concentration to below 2%, and build an inert and sterile preservation environment. For puffed foods, baked goods, dried fruits and other oxygen-sensitive products, nitrogen filling can prevent product crispness reduction and mildew deterioration; for fresh meat, cooked food and quick-frozen products, it can delay protein oxidation and bacterial reproduction, extending the shelf life from several days to several months. Meanwhile, nitrogen is colorless, odorless, non-toxic and chemically inert, which will not react with food ingredients or affect food taste, color and nutritional value, meeting food-grade safety standards.
In addition to excellent preservation effects, membrane separation nitrogen generators have significant industrial application advantages in food processing and production. The equipment has no vulnerable wearing parts, realizes maintenance-free long-term operation, and is suitable for continuous assembly line production of food factories. The start-up speed is fast, and qualified nitrogen can be produced in a few minutes without preheating and long waiting time, matching the high-speed operation rhythm of food packaging lines. Compared with PSA nitrogen generators, membrane equipment has lower operating noise and smaller energy consumption, and will not cause environmental pollution during operation. It is widely used in modified atmosphere packaging of puffed snacks, vacuum nitrogen filling of nut products, sealed storage of grain and oil, and fresh-keeping transportation of fresh food, becoming an indispensable key equipment for standardized and large-scale production in the food industry.