In the refined production system of modern industry, the stability of
nitrogen supply in terms of purity, pressure and flow directly determines
product quality and production safety. It is widely applied in high-end
industries such as electronic semiconductors, new energy lithium batteries, fine
chemical engineering, food preservation, pharmaceutical manufacturing and
metallurgical heat treatment. Most traditional ordinary nitrogen generators
operate in semi-automatic mode, which can only complete basic nitrogen
production without real-time data monitoring, abnormal early warning and
parameter adjustment functions. The operating status and gas quality are judged
purely by manual experience, easily causing problems such as substandard
nitrogen purity, fluctuating air pressure, abnormal flow and no-load energy
consumption. These issues not only result in energy waste, but may also allow
unqualified gas source to flow into the production line, leading to batch
product defects and even potential safety hazards such as explosion and leakage.
As a new generation of intelligent industrial gas supply equipment, the nitrogen
generator system with monitor deeply integrates traditional nitrogen production
technology with intelligent sensing, data acquisition, real-time monitoring,
automatic early warning and intelligent regulation technology. It realizes
visualized, digital and closed-loop automatic control of the entire nitrogen
production process, completely solving the industry pain points of lagging
management, insufficient precision and cumbersome operation and maintenance of
traditional equipment, and has become a standard core equipment for intelligent
industrial gas supply.
The nitrogen generator with monitoring system features core advantages of
accurate real-time monitoring, full-dimensional data management and intelligent
autonomous regulation. The complete system consists of a basic nitrogen
production unit, intelligent sensor acquisition unit, touch display terminal,
data early warning module and automatic regulation module. All units cooperate
and link to realize closed-loop control of the nitrogen production process.
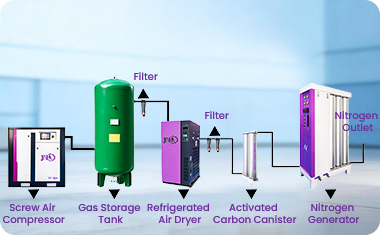
Adopting mature PSA pressure swing adsorption nitrogen production principle, the
equipment takes compressed air as raw material and separates oxygen, water vapor
and impurities through molecular sieve adsorption to produce high-purity
industrial nitrogen. On this basis, it is equipped with high-precision
multi-dimensional sensors to continuously collect more than ten key operating
parameters for 24 hours, including nitrogen purity, output flow, gas supply
pressure, inlet temperature, air dew point, equipment operating load and filter
element status, completely eliminating the management blind spots of traditional
nitrogen production equipment without data recording or early warning. All
collected data is transmitted to the high-definition touch display terminal in
real time and presented intuitively in the form of numbers, curves and reports,
enabling operators to master equipment operating status and gas source quality
without manual detection and recording.
Gas purity monitoring is the core function of the intelligent system and
the key to ensuring industrial production quality. Equipped with a
high-precision oxygen sensor analyzer, the equipment accurately converts
nitrogen purity by detecting residual oxygen concentration in real time,
covering the full purity range from 95% to 99.999% to meet the precise gas
supply standards of different industries. Compared with the hysteresis and
errors of traditional manual sampling detection, the intelligent monitoring
system realizes millisecond-level data updates and uninterrupted full-process
monitoring to avoid purity fluctuation and excessive residual impurities. Once
the nitrogen purity drops below the preset production threshold, the system will
immediately trigger an acousto-optic alarm and start the emergency protection
mechanism automatically, switching the waste gas bypass or shutting down the gas
output to prevent unqualified nitrogen from entering the production pipeline and
avoid product quality risks from the source. It is perfectly suitable for
high-standard gas supply scenarios such as semiconductors, precision electronics
and pharmaceuticals. Meanwhile, the system supports full-process data storage
and traceability, automatically generating operation reports for enterprise
production quality inspection, compliance filing and process optimization.
In addition to purity monitoring, the system realizes full-dimensional
intelligent management of pressure, flow, temperature and equipment working
conditions. In terms of pressure monitoring, it tracks inlet pressure,
adsorption tower working pressure and gas storage tank stabilizing pressure in
real time, automatically adjusting the adsorption and pressure relief rhythm to
avoid equipment damage caused by overpressure and insufficient gas supply caused
by low pressure, ensuring constant and stable output air pressure. The flow
monitoring module accurately counts instantaneous gas production flow and
cumulative total output, helping enterprises accurately calculate gas
consumption costs, optimize production capacity ratio and avoid energy waste
caused by no-load and excessive gas production. The temperature and dew point
monitoring functions detect equipment operating temperature and gas dryness in
real time, timely identifying problems such as blocked filter elements, damp
molecular sieves and excessive water and oil content in compressed air to avoid
equipment failures in advance. Furthermore, the built-in equipment
self-diagnosis program detects the operating status of circuits, air circuits
and valves in real time to accurately locate fault points, eliminating the blind
troubleshooting of traditional equipment and greatly reducing operation and
maintenance difficulties.
Intelligent early warning and remote management significantly improve
equipment operation safety and unattended operation capability. The nitrogen
generation system is equipped with a comprehensive abnormal early warning
mechanism, which can realize advance reminder, real-time alarm and automatic
protection for various faults including insufficient purity, abnormal pressure,
over-temperature overload, failed filter elements, pipeline leakage and expired
consumables. It supports custom parameter setting, allowing enterprises to
independently set the upper and lower limits of purity, pressure and temperature
according to production process requirements to meet personalized production
needs. High-end models are equipped with a remote monitoring system, enabling
real-time remote viewing of operating data, remote adjustment of operating
parameters and fault push notifications through mobile and computer terminals.
It realizes 24/7 remote operation and maintenance without on-duty personnel,
greatly saving labor costs and adapting to the automatic and unattended
production mode of modern factories. Meanwhile, the system features data memory
and power-off protection functions, automatically restoring preset operating
parameters after power failure restart to ensure production continuity and avoid
working condition disorder.
In terms of operation, maintenance and energy consumption optimization, the
intelligent monitoring nitrogen generator has incomparable cost performance
advantages over traditional equipment. Traditional nitrogen generators require
regular manual inspection, manual parameter detection and blind periodic
consumable replacement, resulting in high operation and maintenance costs and
low efficiency. In contrast, the intelligent monitoring system accurately
prompts the service life and replacement cycle of consumables, realizing
on-demand replacement to avoid excessive or delayed maintenance and effectively
reduce consumable costs. Meanwhile, based on real-time working condition data,
the system intelligently adjusts equipment operating load and dynamically
optimizes gas production efficiency according to production line gas demand,
eliminating no-load and light-load energy waste. Its energy-saving efficiency is
more than 25% higher than that of ordinary nitrogen generators, greatly reducing
enterprise power consumption costs in long-term operation. Adopting a modular
integrated design, the equipment operates stably with a low failure rate,
supports 24-hour uninterrupted continuous operation, and features longer service
life and lower comprehensive operation and maintenance costs.
Modern industrial production is rapidly upgrading toward intelligence,
digitization and precision, and traditional extensive nitrogen production
equipment can no longer meet high-end production requirements. Integrating
precise nitrogen production, real-time monitoring, intelligent regulation,
safety protection and efficient operation and maintenance, the nitrogen
generator system with monitor effectively solves industrial pain points such as
unstable gas supply, substandard purity, high energy consumption, cumbersome
maintenance and frequent potential safety hazards. It can accurately adapt to
working conditions for both ultra-high-purity gas supply in precision
manufacturing and large-scale gas supply in general industries, providing strong
equipment support for enterprise safety production, quality control and cost
reduction and efficiency improvement. It represents the inevitable trend and
mainstream choice of intelligent upgrading in the industrial nitrogen production
field.